What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
What we cover
Best CNC Drill Bits: Compare Types, Sizes, and Materials
For most CNC woodworking, choose a solid-carbide, two-flute brad-point bit for clean holes in solid wood, a carbide compression bit when drilling through plywood or veneered panels, and a carbide twist drill for general-purpose holes where the machine can clear chips reliably. Before buying, match the bit’s shank to the machine’s collet, its cutting geometry to the material, and its length and diameter to the hole you need.
Which CNC drill bit fits your job?
“CNC drill bits” covers several geometries rather than one universal tool. A bit that makes a crisp hole in maple may tear the face veneer of plywood; one that clears chips well in a deep hole may leave a less tidy entry. Use the comparison below as a starting point. Dimensions are common examples, not universal standards, so confirm the specifications of the exact bit and machine.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.


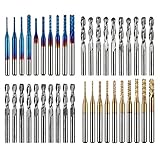
| Bit style | Typical sizes | Best suited to | Chip evacuation and edge quality | Shank and durability notes |
|---|---|---|---|---|
| Brad-point twist drill | 3–12 mm diameter; 6–10 mm shank | Solid wood, pilot holes, dowel holes | Point helps locate the hole; flutes lift chips, but deep holes need pecking | Often sold in HSS or carbide; match the shank to the collet |
| Standard twist drill | 1–13 mm diameter; commonly 6 mm or 1/4 in shank | Wood, plastics, and some nonferrous materials when specified | Versatile flutes; chip packing is possible in deep or resinous wood | HSS costs less; carbide resists wear better but is more brittle |
| Through-hole / dowel drill | 5–15 mm diameter; 6–10 mm shank | Repeated joinery holes and deeper boring | Geometry varies; some designs clear chips efficiently, while others need retract cycles | Check whether it is intended for CNC rotation and the machine’s feed direction |
| Compression drill | 3–8 mm diameter; commonly 6 mm or 1/4 in shank | Plywood, veneer-faced panels, laminates | Opposing cutting directions can reduce tear-out on both faces when the cut depth suits the geometry | Usually carbide; requires correct engagement depth and rigid workholding |
| Forstner-style bit | 10–50 mm diameter; shanks vary widely | Flat-bottomed, wide holes in wood | Produces a flat-bottomed recess, but wide cutters create more heat and chip load | Verify that the CNC spindle, collet, and toolpath support its shank and diameter |
Choose by material and required accuracy
Solid wood
For accurate dowel or hardware holes, a brad-point drill is a dependable choice: its center point helps keep the bit from wandering at entry. Carbide is useful for frequent production or abrasive stock, while HSS can be a sensible lower-cost option for occasional work. In either case, use a peck-drilling cycle for holes deep enough that chips stop clearing freely. Packed chips generate heat, dull edges faster, and can leave a rough or oversized hole.
Plywood and veneered panels
Face veneer is prone to splintering, particularly where the bit exits. A compression drill can improve both-face quality if its upcut and downcut portions engage the panel faces as intended. That depends on panel thickness, the tool’s compression zone, and the programmed depth—not just the label. For a thin panel or a blind hole, a brad-point or suitable downcut geometry may be a better fit. Test on offcuts from the same panel before drilling a visible part.
MDF, plastics, and other materials
For MDF, carbide generally holds an edge longer than HSS because the material is abrasive. Dust extraction matters: fine MDF dust can collect around the cut and obscure chip-clearing problems. Plastics vary considerably; use a bit specifically suited to the plastic and avoid letting chips melt onto the cutting edge. Metal drilling requires a bit, spindle speed, feed, and workholding appropriate to that metal—woodworking drill settings are not a safe assumption.
Shank fit, diameter, and depth: check before ordering
- Shank: A 6 mm shank will not fit a 1/4-inch collet correctly, and the reverse is also true. Use the exact collet size specified by the machine; never force a near-match or rely on an adapter that is not rated for the setup.
- Diameter: Select the finished hole size, allowing for the bit’s stated diameter and the machine’s runout. For a precision dowel fit, make a test hole and check the actual dowel rather than assuming a nominal size guarantees a snug fit.
- Length: Use the shortest cutting length that reaches the required depth. A long, slender bit deflects more, which can affect hole position and diameter.
- Bottom shape: Twist drills typically leave a pointed or conical bottom. For a flat-bottom recess, choose a suitable Forstner-style or other flat-bottom cutter and confirm it is rated for CNC use.
- Runout and clamping: Clean the collet and shank, seat the tool properly, and clamp the work securely. Dirt, a worn collet, or a loose panel can undermine accuracy even with a new bit.
Make the choice by use frequency and budget
| Your situation | Practical choice | Trade-off to expect |
|---|---|---|
| Occasional home projects, mostly softwood | HSS brad-point bits in the diameters you use most | Lower initial cost, but edges wear sooner in abrasive materials |
| Frequent MDF or plywood work | Carbide bits; add compression geometry for suitable through-cuts | Higher purchase cost; brittle edges can chip if dropped or misused |
| Repeatable dowel joinery | Carbide or quality HSS brad-point bits matched to the dowel sizes | Test fit and maintain consistent depth and workholding |
| Mixed materials and limited tool storage | A small set of common diameters plus material-specific bits as needed | A general-purpose bit is convenient, but won’t optimize every material |
As a simple sizing example, if a project calls for a 6 mm dowel, start with a bit specified at 6 mm, then drill a test hole in matching scrap. If the dowel binds, check for runout, chip-packed walls, and material swelling before changing the programmed diameter. A tiny adjustment in the toolpath can affect fit, so record the successful setting for repeat parts.
Ownership: what wears first and how to extend bit life
Cutting edges are the main wear point; resin buildup can make a bit cut poorly before the edge is truly dull. Inspect the flutes for packed dust, resin, chipped carbide, or a polished, rounded edge. Clean the bit with a product appropriate for its material and dry it before storage. Avoid striking carbide bits against the table or collet—they resist abrasion but can fracture from impact.
Use the machine manufacturer’s guidance for spindle speed and feed, and reduce chip load or use pecking when chips do not clear. A slow feed is not automatically gentler: rubbing can create heat and accelerate wear. If a hole starts burning, wandering, or coming out rough, pause and check chip evacuation, tool sharpness, runout, and workholding before compensating with a larger bit.
Bottom line
For clean solid-wood joinery, start with a brad-point CNC drill bit in the exact shank and hole size your machine accepts. For plywood and veneer, consider a compression bit only when the panel thickness and cutting geometry align. Choose carbide for frequent or abrasive work, HSS for economical occasional use, and prioritize short reach, clean chip evacuation, and a test hole whenever fit or surface quality matters.